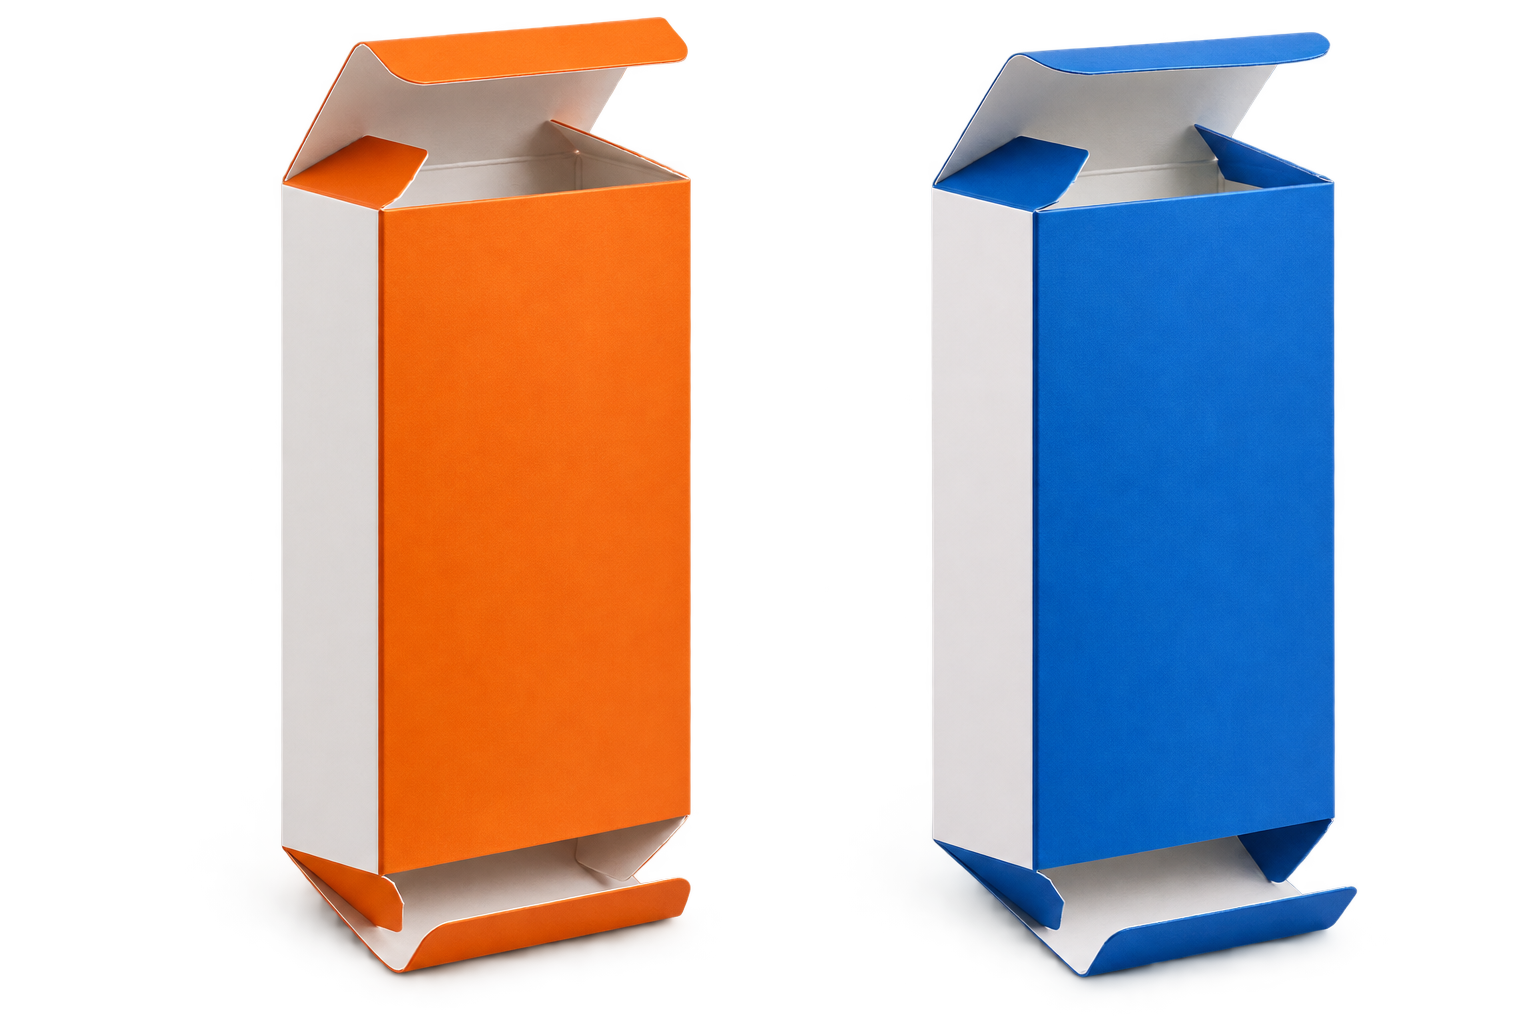
Sequenced base flaps
Operators fold the numbered or understood flap sequence so the final panel locks the base together.
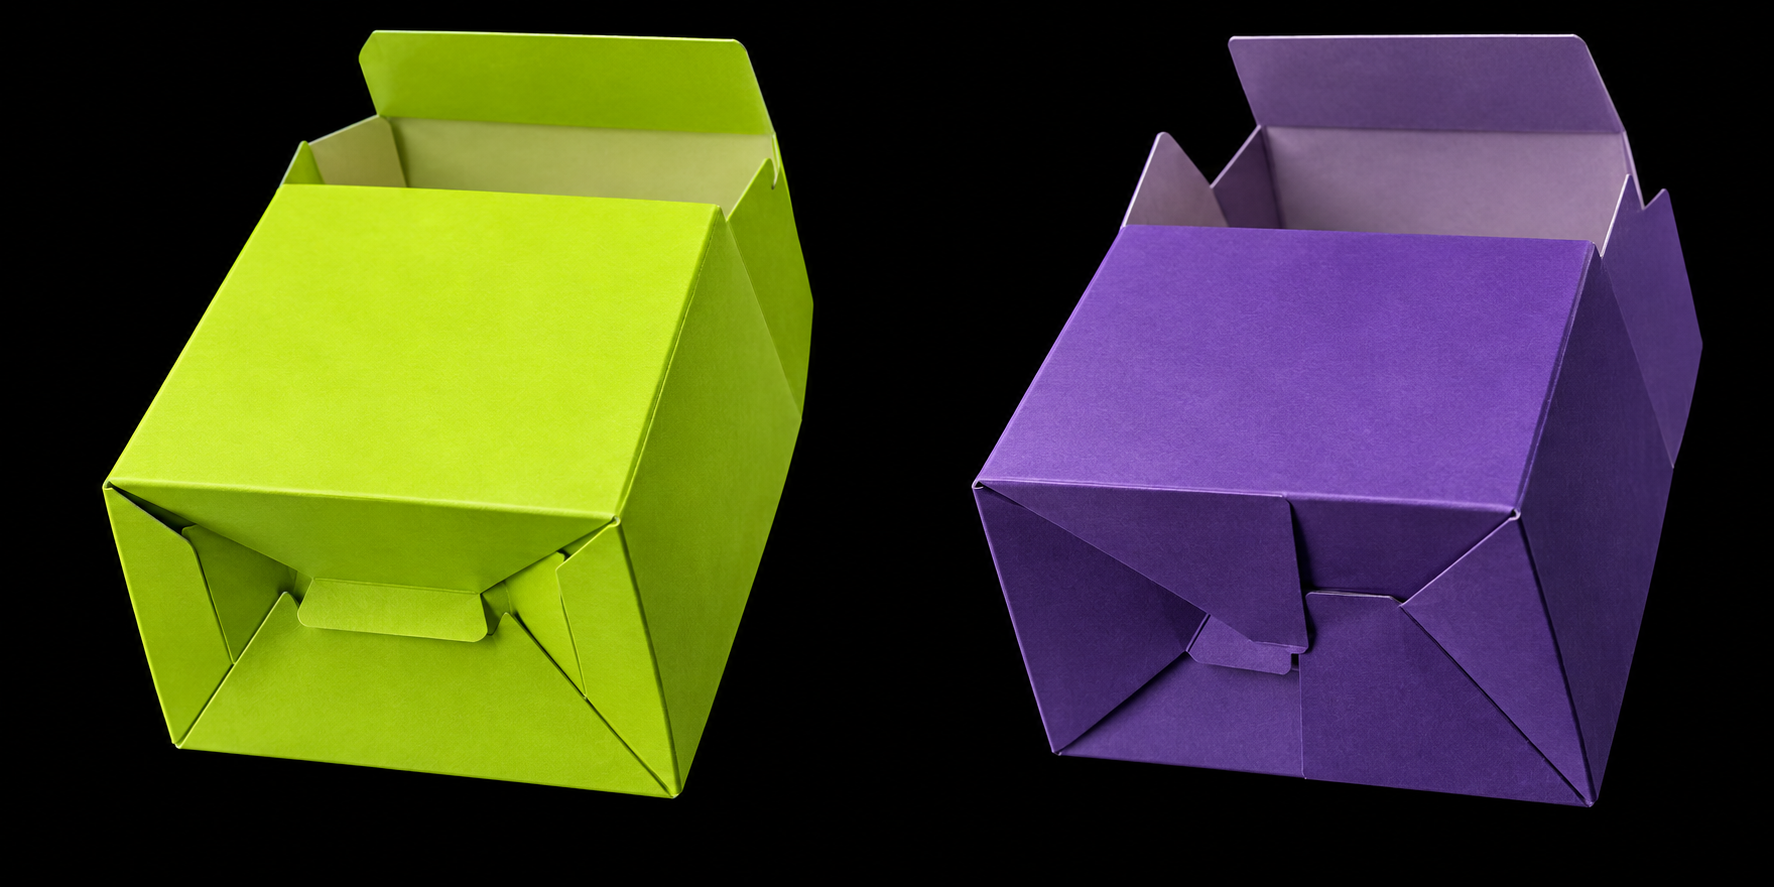
Snap-lock bottom cartons, sometimes called 1-2-3 bottom cartons, use interlocking base flaps to provide more support than a standard tuck closure. The format is useful for candles, bottles and heavier retail items packed by hand.
An interlocking-base carton assembled in sequence for dependable support without a pre-glued base.
Snap-lock bottom cartons use a set of base flaps that interlock in sequence, often described as a 1-2-3 bottom. Unlike a crash-lock carton, the base is not automatically formed by pre-glued panels. The format arrives flat, gives more support than a basic tuck base and suits hand-packed products where a deliberate assembly step is acceptable.
Operators fold the numbered or understood flap sequence so the final panel locks the base together.
The base gains support from overlapping board geometry rather than an automatic pre-glued base assembly.
The top remains easy to fill, close and reopen while the locked base carries the product.
The box style, board, product and packing process need to work together. These are the advantages to use—and the points to verify before production.
Interlocking flaps create a supportive base without automatic-base gluing.
The structure arrives flat, helping with storage before packing.
It offers a useful balance of protection, presentation and production economy.
Account for the extra packing time and give operators a clear, repeatable base-folding sequence.
Physically test the packed carton because weight capacity changes with dimensions, board and flap geometry.
Check the underside for a level, secure lock where the carton must stand upright on shelf.
Review whether a crash-lock base is more suitable when packing speed becomes the dominant requirement.
Candles, glass bottles, jars and heavier retail. Final suitability is confirmed against the packed product and distribution route.
Stiffness, print response, fold performance and product weight shape the material decision. These are the most relevant starting routes for this structure—not fixed specifications.
A practical route for moderate product weights where stiffness and a high-quality print face are needed.
Supports premium graphics and clean internal presentation for candles, bottles and personal-care products.
Can be evaluated when natural appearance, recycled content or additional strength is part of the brief.
Product-specific combinations to evaluate before opening the complete interactive library.
Helps control scuffing on dark colours and high-contact retail packs.
Adds controlled premium accents without interfering with the locking base.
Creates tactile hierarchy on principal panels where reverse-side relief is acceptable.
Can reveal a candle, bottle or jar while maintaining safe board margins and tested rigidity.
Click through premium finishing and structural add-ons for snap-lock bottom cartons. Each option shows the visual character, best use and production point to resolve before artwork approval.
Gold and silver foil are shown separately. Foiling is also available in a wide choice of metallic and pigment colours, subject to the selected foil range and stock.
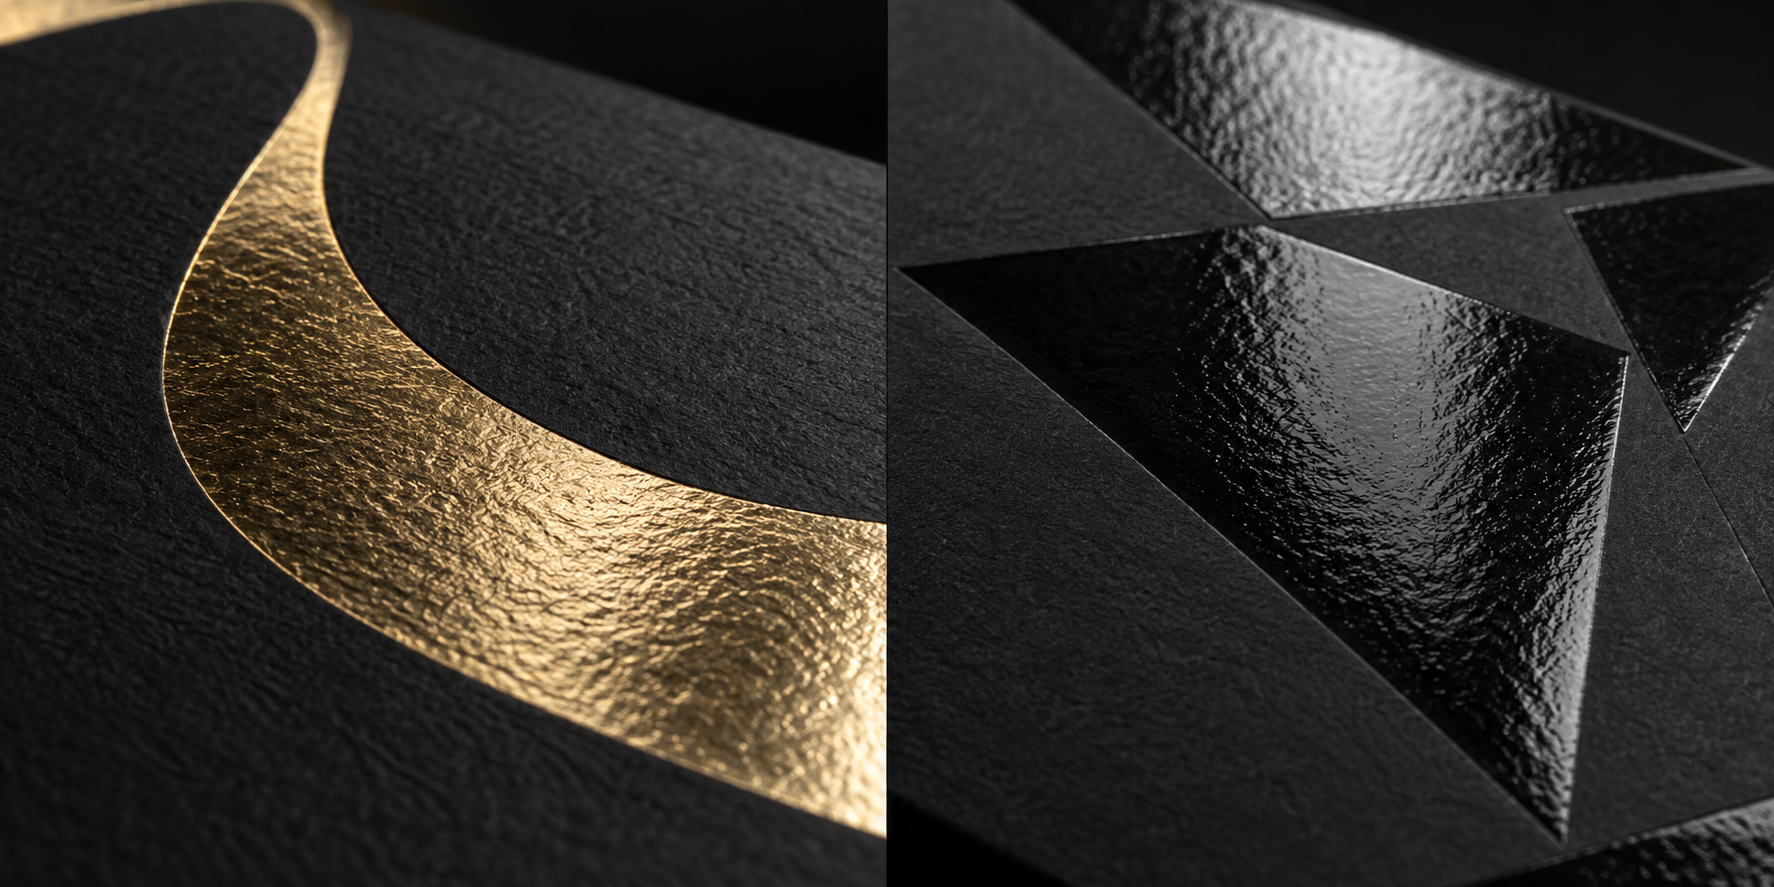
Warm metallic reflection
A heated die transfers gold-coloured foil onto selected artwork, creating a crisp reflective focal point without printing an additional ink colour.
A screen can suggest colour and surface, but fit, fold and finish should be judged against the actual structure. For a snap-lock bottom carton, the approval route can include a plain prototype, printed sample or finish reference.
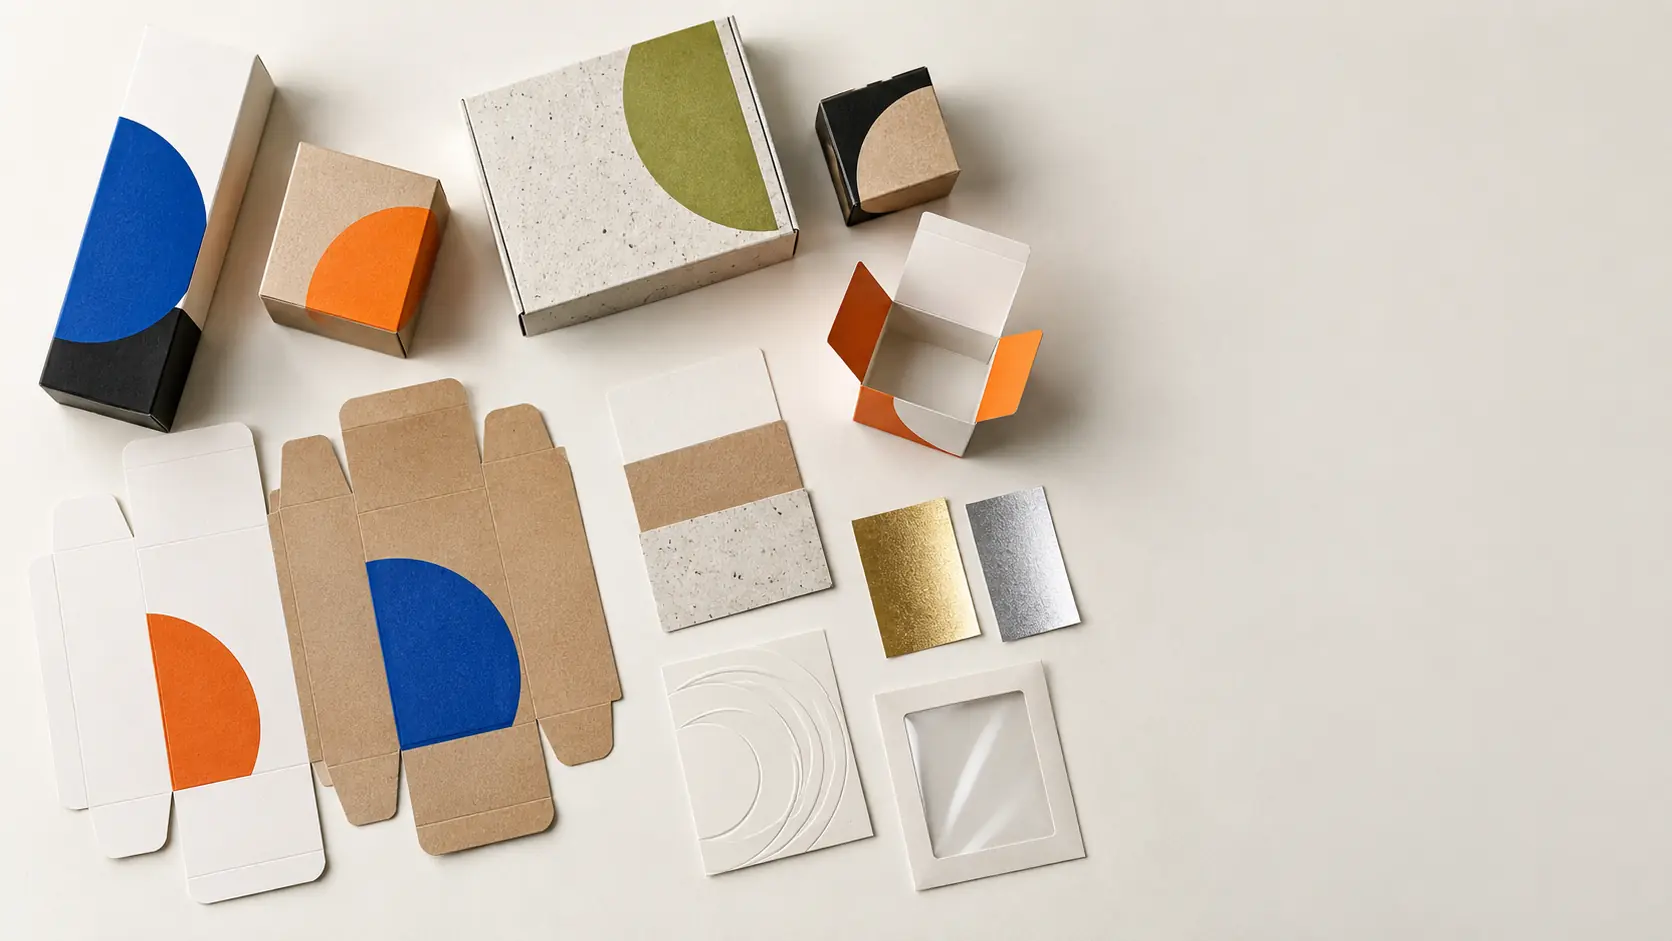
Confirm the internal dimensions, product movement and the way each panel opens and closes.
Review stiffness, fold response, colour and small copy on the chosen paperboard route.
Check foil, relief, varnish, windows or inserts against the live dieline and tolerance.
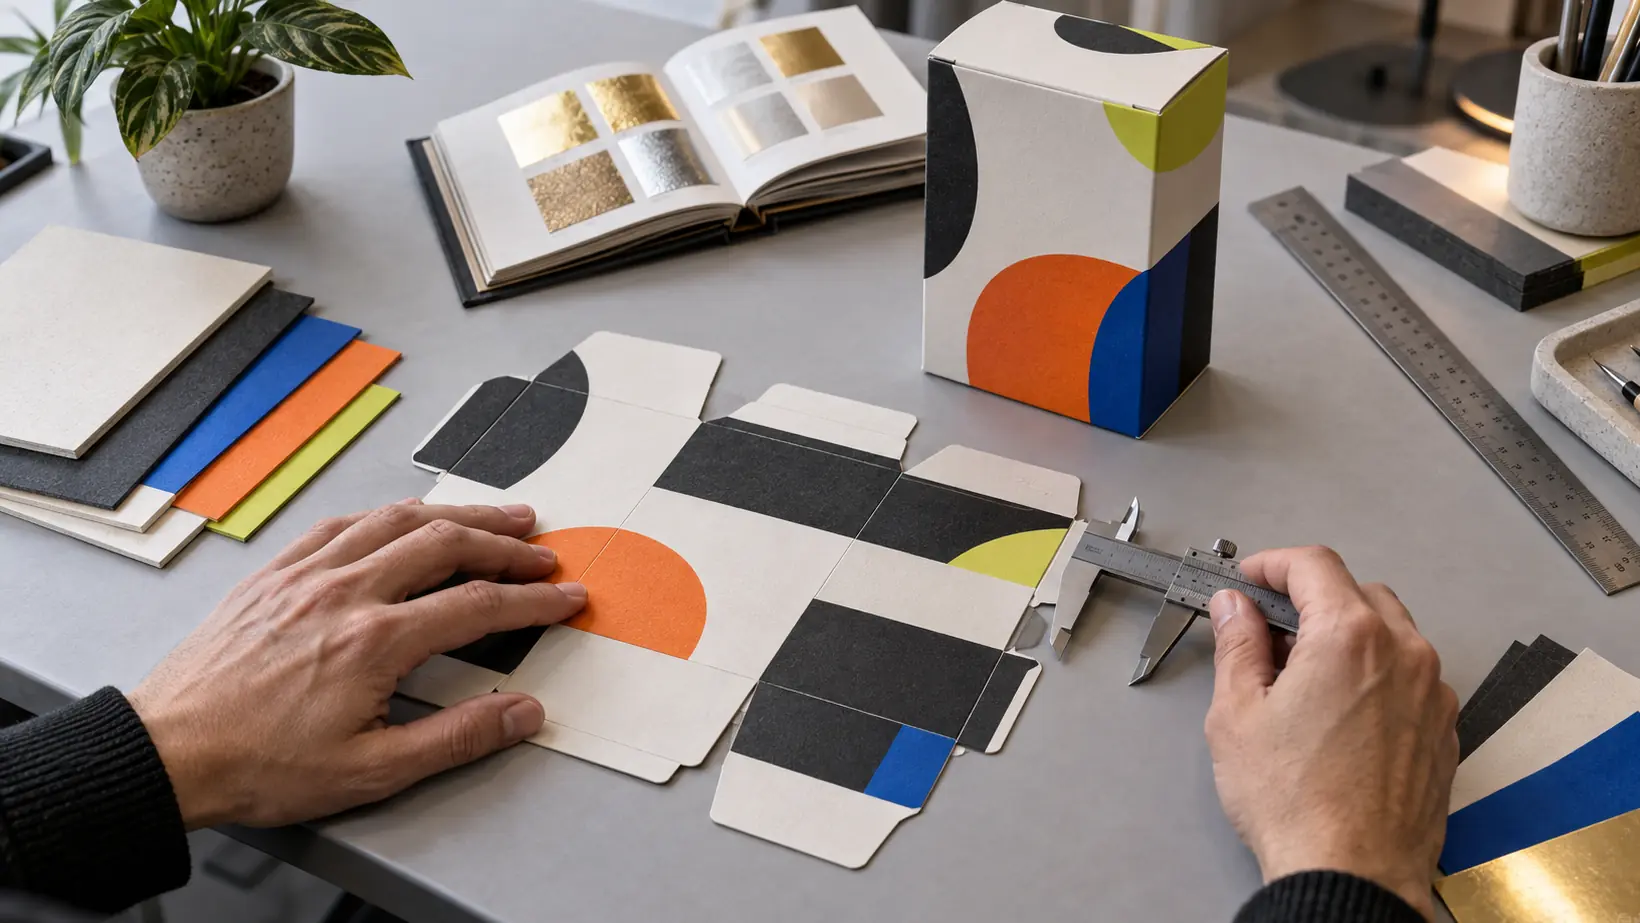
Images are illustrative specification visuals, not client work. The finished result is developed and approved against your product, dieline, board and artwork.
Confirm dimensions, weight, quantity, orientation, packing method and delivery destination.
Select or develop the dieline, board route, closure and any required internal support.
Review fit and opening behaviour with a structural or printed sample where the brief requires it.
Check copy, colour, barcode position and each finishing layer on the approved dieline.
Allow a typical 7–10 working days after the final specification and artwork are approved.
Plan transit separately against packed volume, destination and the required arrival date.
Structure, quantity, timing, print and packing answers for this carton format.
Snap-lock bottom cartons, sometimes called 1-2-3 bottom cartons, use interlocking base flaps to provide more support than a standard tuck closure. The format is useful for candles, bottles and heavier retail items packed by hand.
Candles, glass bottles, jars and heavier retail. Final suitability depends on the item dimensions, weight, fragility and the way it will be packed and transported.
Yes. The approved dieline can carry brand colour, product information, barcodes and imagery, with foil, emboss, deboss, spot UV, lamination or windows added where the material and artwork allow.
Yes, where the panel size and carton structure allow. A die-cut aperture can be left open or backed with a clear window patch. Patch material, overlap, glue area, product protection and recycling objectives are confirmed for the specific application.
Gold and silver are the most familiar choices, but hot foil is available in many metallic and pigment colours, including copper, rose gold, red, blue and green, plus selected holographic effects. The final colour and sheen are chosen from physical swatches and remain subject to supplier range and stock.
The minimum order quantity starts at 500 units. Finished size, board, print coverage and finishing requirements are confirmed before the production route is priced.
Typical production lead time is 7–10 working days after the structure, artwork, paperboard and finishes are approved. Structural development, sampling and delivery are additional where required.
The base flaps are folded in a defined sequence before the final flap locks the assembly. The exact order follows the approved carton construction.
A snap-lock base is manually interlocked during packing. A crash-lock base is pre-glued and forms as the carton is opened, usually making erection faster.
Yes. The glued carton body is normally delivered flat, and the interlocking base is assembled when the product is packed.
Share the product dimensions and quantity now. Board, structure, finishes and add-ons can be refined during the specification review.